·Extreme‑Length Forming Technology
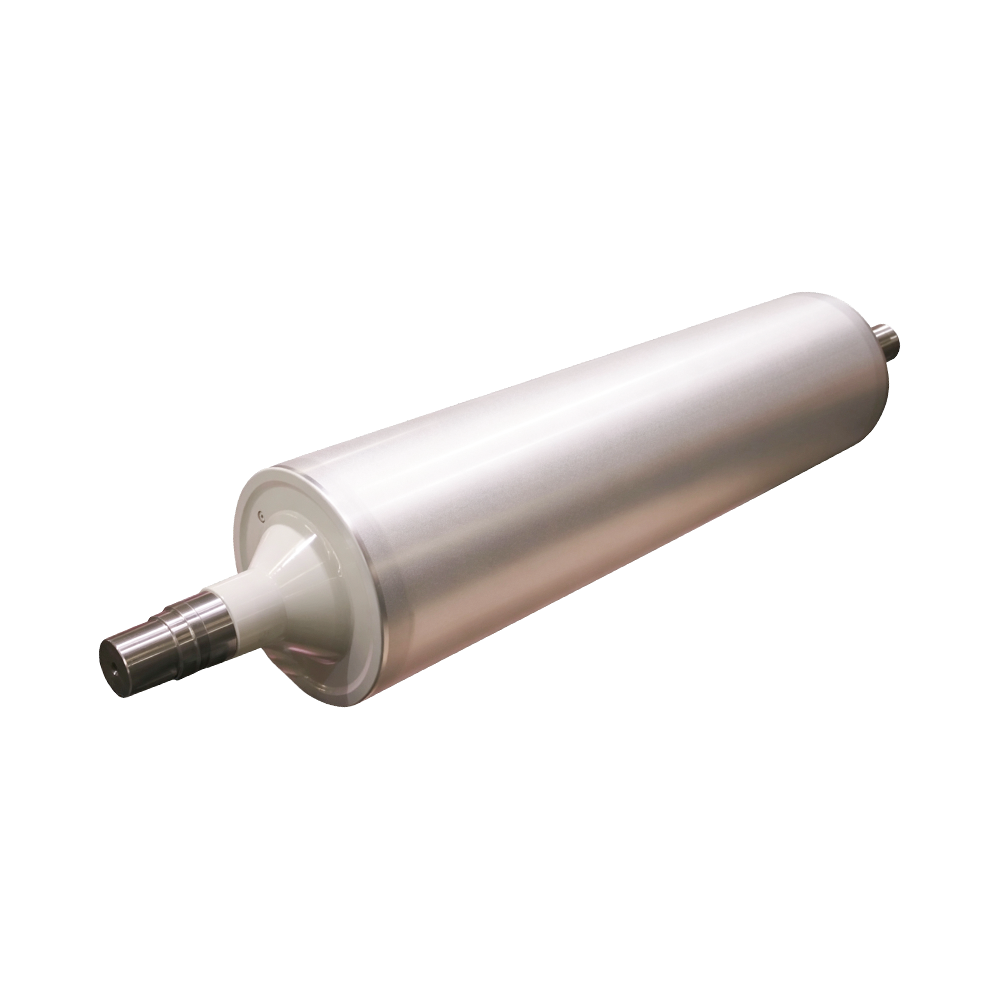
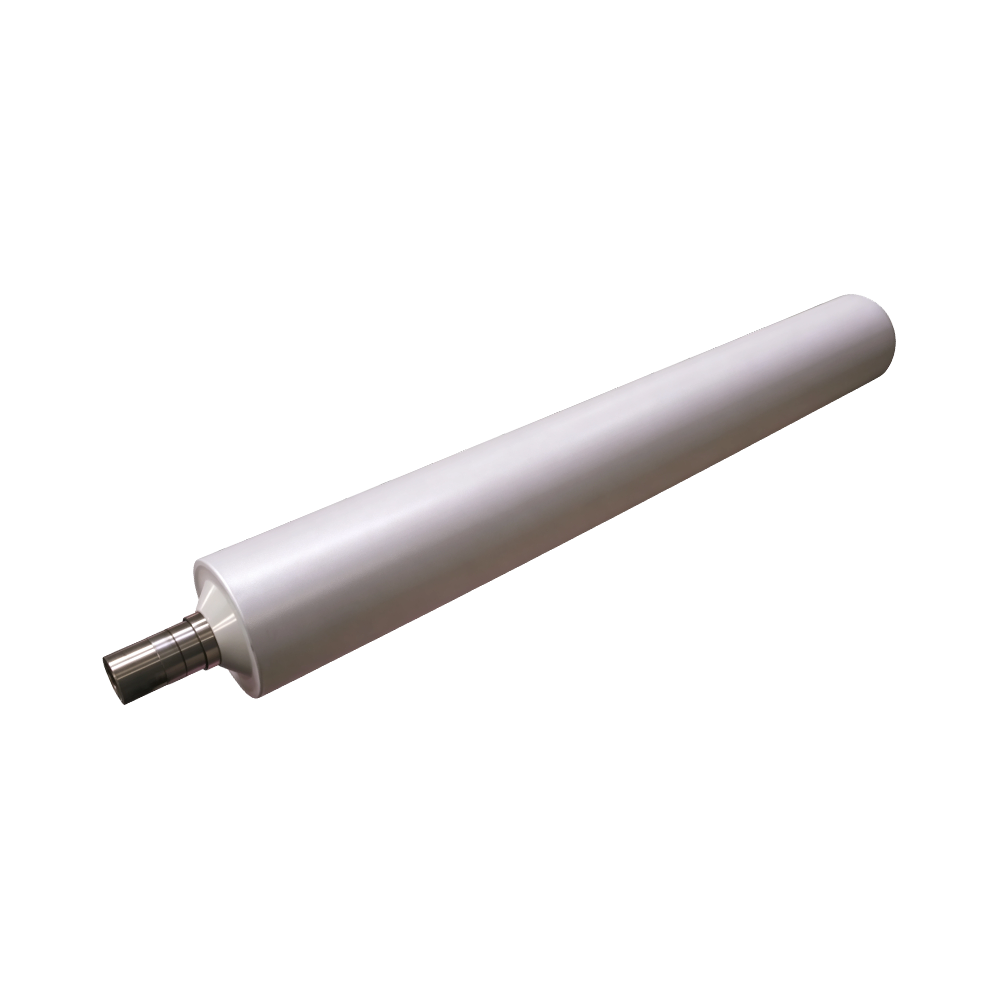
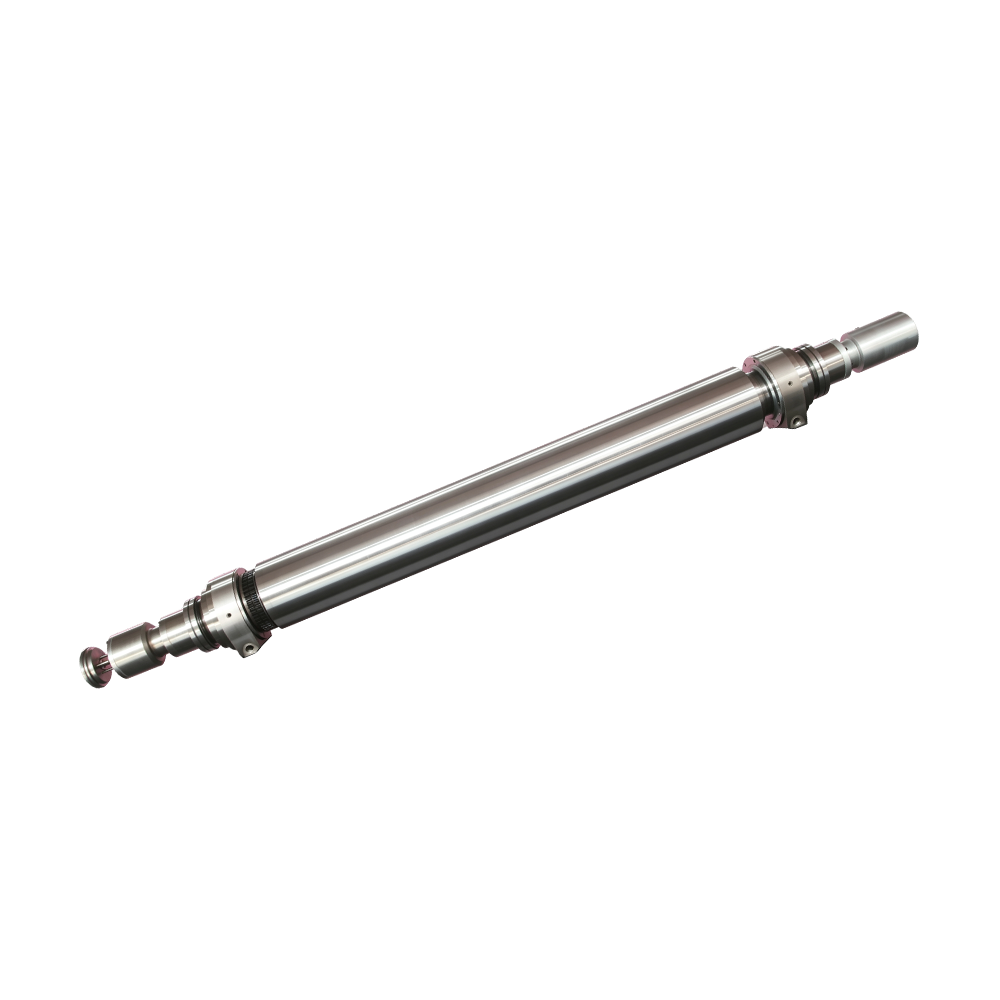
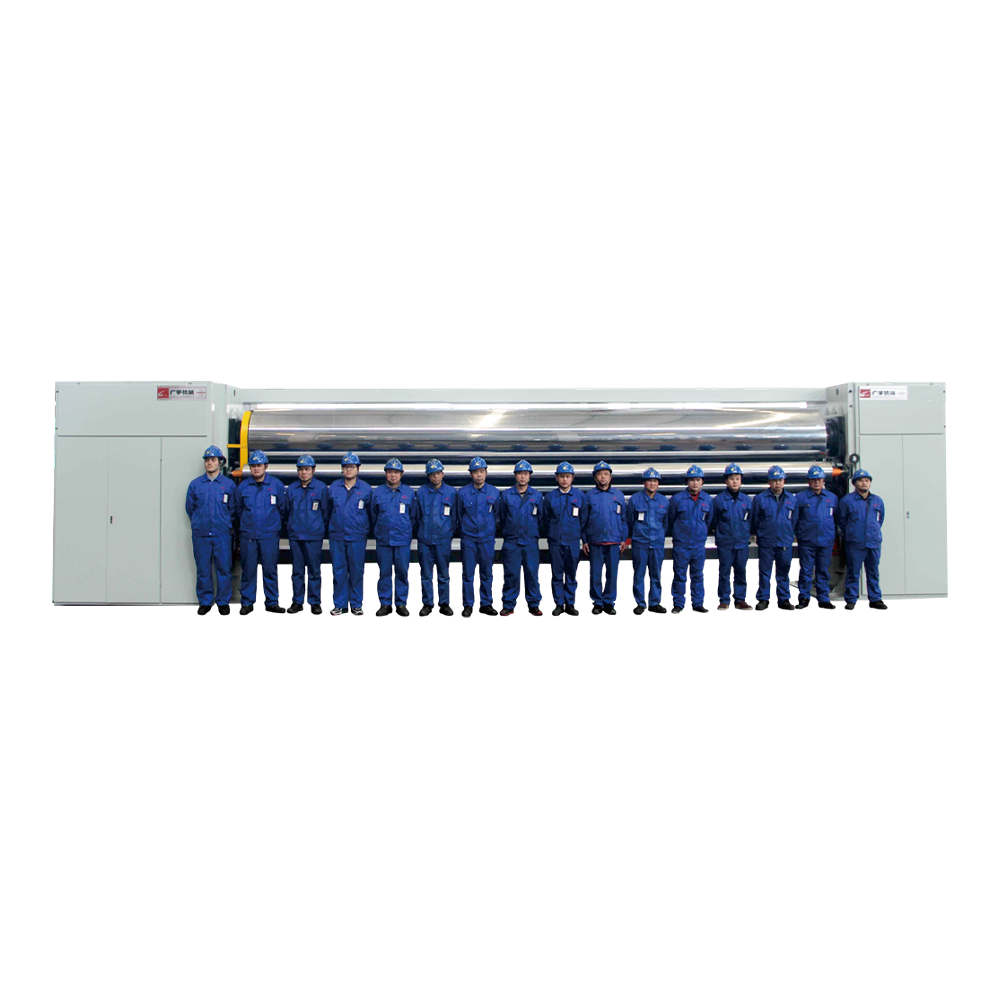
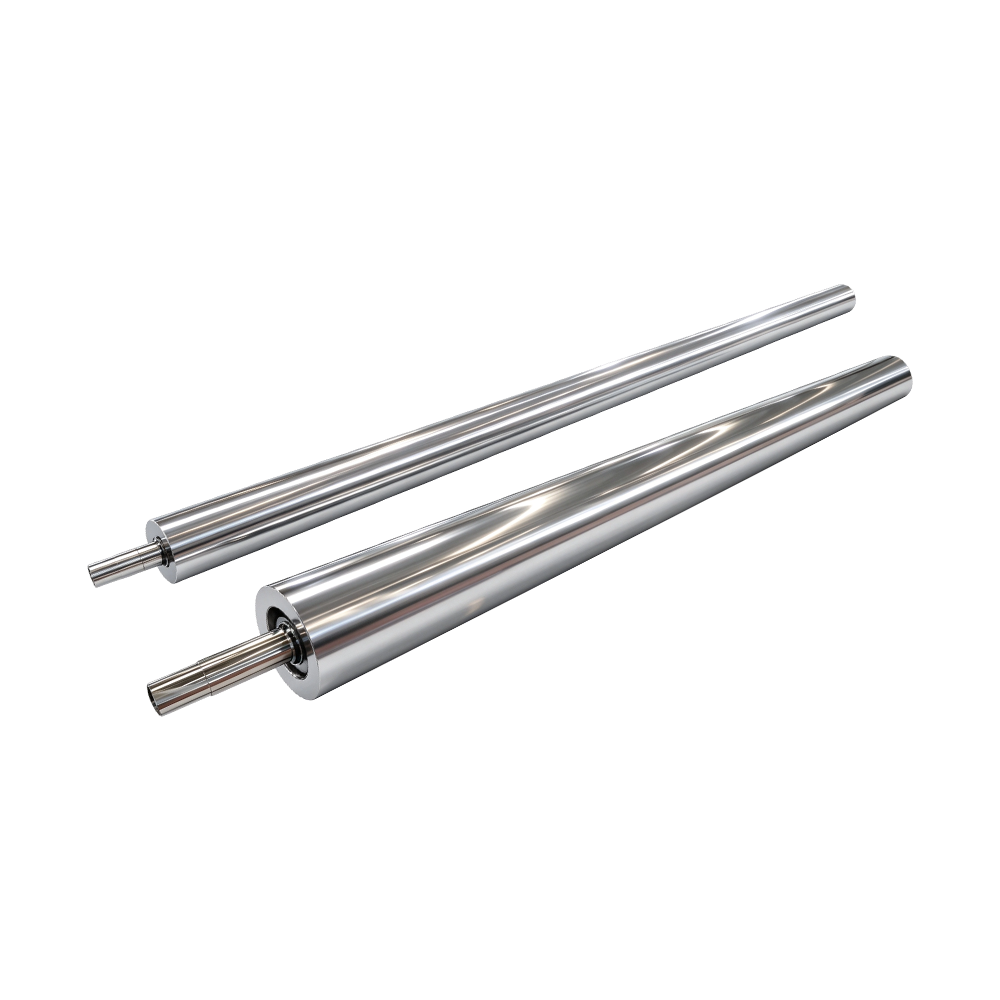
Maximum specifications reach Φ900 mm × 16 000 mm effective face length with an optimised length‑to‑diameter ratio that controls natural deflection under heavy‑load high‑speed operation. Ordinary manufacturers typically use segmented welded construction for extra‑long rollers, resulting in weld stress concentration, deformation under long‑term operation, and rapid concentricity failure. The thick‑wall seamless shell with internal stiffening ribs and multi‑stage finite‑element stiffness simulation optimisation ensures a fully integrated roller body with no welded seams, suitable for long‑distance web handling in BOPP, BOPET, BOPA, BOPE, and lithium battery separator ultra‑wide lines, resolving the common industry problems of centre sagging and transverse tension non‑uniformity on guide rollers exceeding 10 metres in length.
·Multi‑Stage Stress‑Relief Process for Extra‑Long Rollers
Achieves static concentricity ≤0.05 mm, with temperature‑controlled versions maintaining whole‑roller surface temperature differential ≤±1.5 ℃ and resistance to deformation under continuous operation. To address internal stress challenges from extra‑long roller machining and alternating hot‑cold cycles, a three‑stage stress‑release process is implemented: rough‑machining aging, finishing vibration aging, and heat‑treatment stabilisation. For temperature‑controlled extra‑long guide rollers, precision‑machined internal spiral heat‑exchange channels ensure uniform thermal fluid circulation, preventing local thermal bowing under high‑temperature stretching. Film longitudinal traction maintains consistent tension without intermittent fluctuations, eliminating longitudinal streaks and thickness deviation defects.
·Thick Dense Hard Chrome Mirror Surface
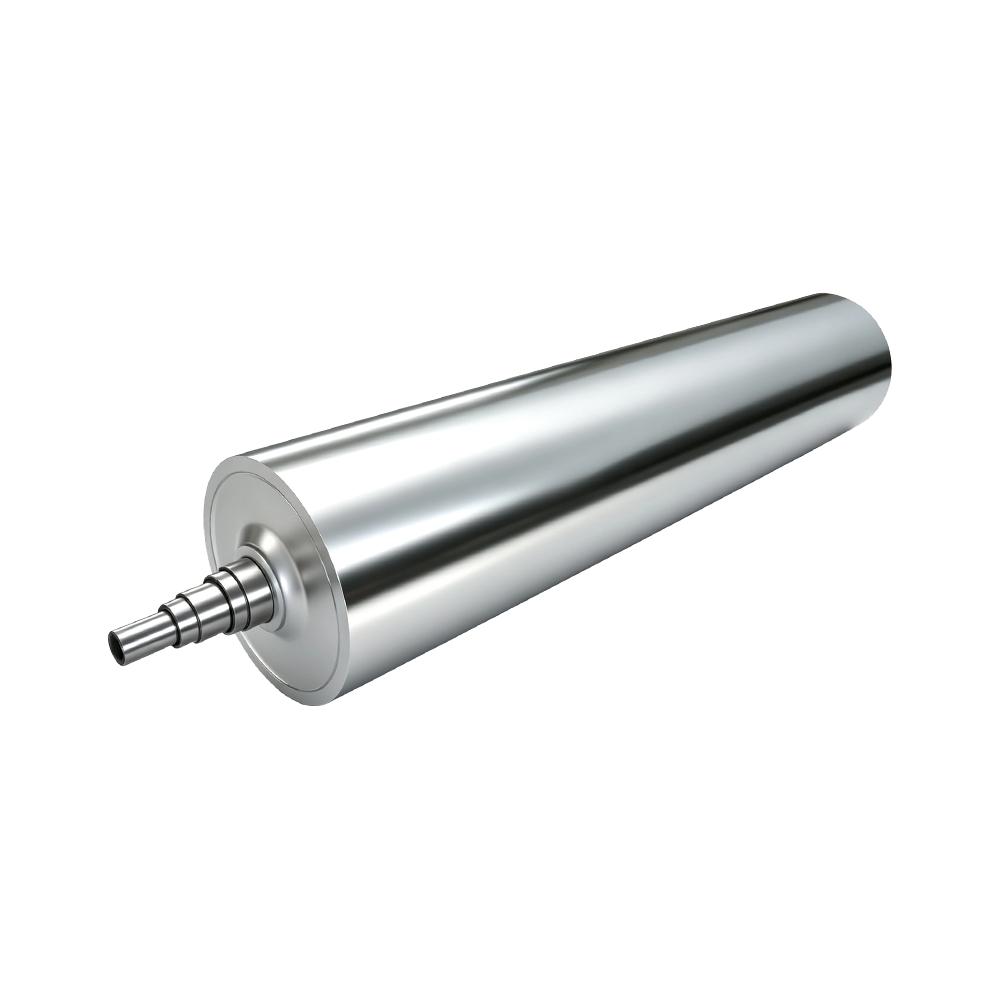
Chrome layer thickness ≥0.10 mm with mirror polish Ra≤0.01 μm, providing low‑friction, scratch‑free contact for ultra‑thin substrates. The fully automated continuous electroplating line deposits a hard chrome layer with metallurgical bonding to the substrate, resistant to peeling. Ultra‑precision mirror polishing eliminates microscopic protrusions. Specifically designed for easily scratched webs including BOPA, lithium battery separators, and ultra‑thin optical films, the roller surface prevents scratches and electrostatic abrasion during high‑speed film sliding, while resisting corrosion from film additives and extraction chemicals. Simple cleaning maintenance and wear service life are 85 % longer than conventional chrome‑plated guide rollers.
·Dual‑Plane High‑Precision Dynamic Balancing for Extra‑Long Dimensions
Supports continuous operation up to 220 m/min with reduced bearing wear and machine vibration. Extra‑long guide rollers on the market typically simplify dynamic balancing procedures, resulting in significant vibration at high speed and bearing failure every 3–6 months. Large‑scale horizontal dynamic balancing equipment implements dual‑plane balancing calibration on both ends of 8–16 metre extra‑long rollers. Significantly reduced operational vibration extends the service life of bearings and machine frames at both ends, reduces scheduled maintenance shutdown frequency, and supports 24/7 uninterrupted production in overseas factories.
·Modular Customisation
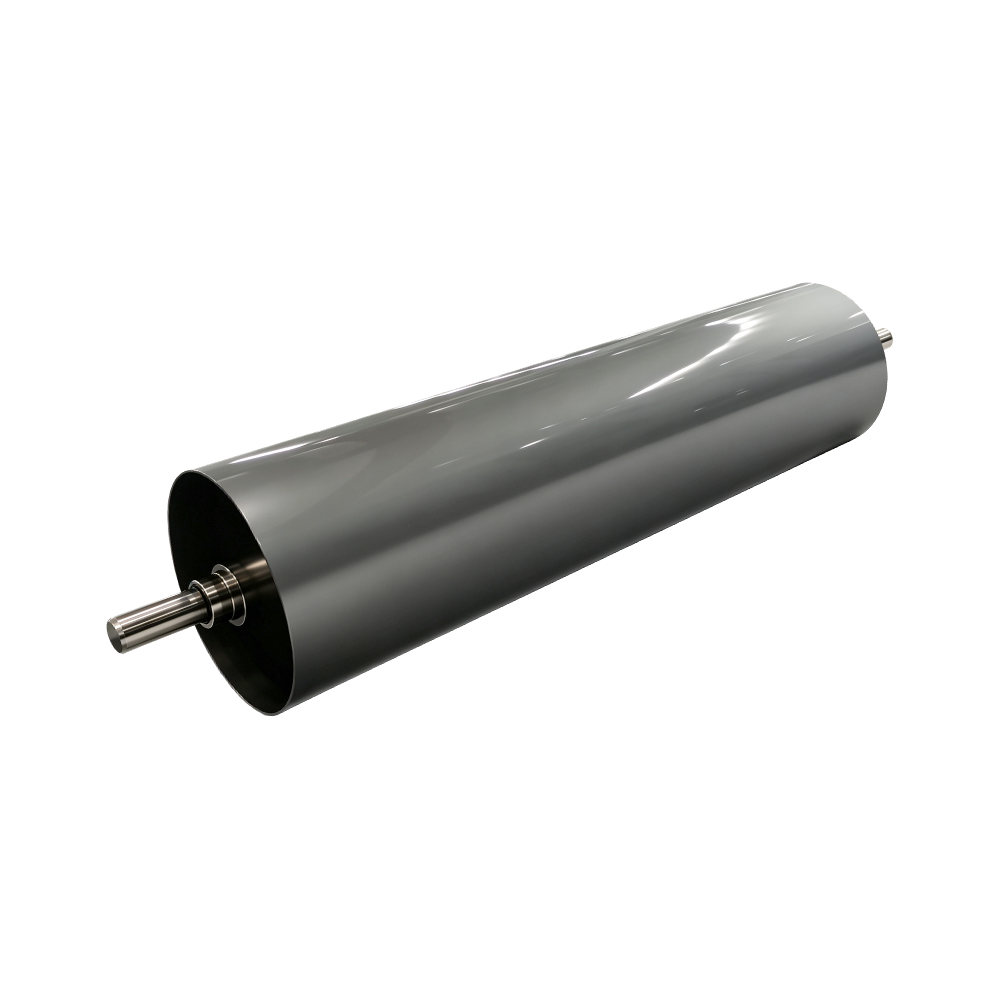
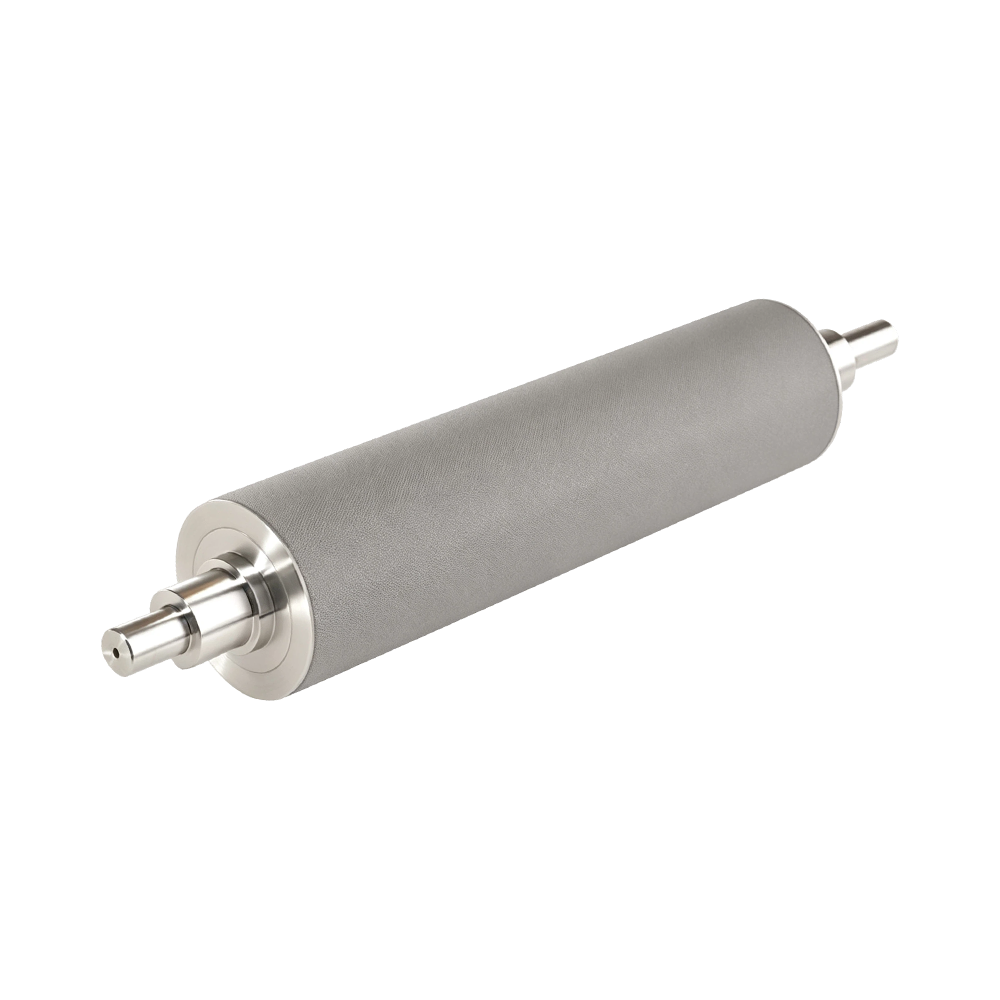
Three configuration options are available: standard plain guide rollers, temperature‑controlled guide rollers with integrated heating/cooling capability, and anti‑stick coated guide rollers, matching stretching, extraction, and slitting processes. Breaking through the industry limitation that extra‑long guide rollers can only produce basic plain rollers, the design integrates spiral flow channels for temperature control, with surface finish options including mirror chrome, matte/satin chrome, and food‑grade anti‑stick coatings. Journal flanges, keyways, and drive interfaces directly match imported biaxial orientation equipment and lithium battery separator extraction units without customer equipment base modification.
·Structural Reliability
Extra‑long guide rollers handle long‑distance web guiding and tension transfer. Once roller bending or concentricity drift occurs, the entire roll of film faces significant scrap risk. The low‑cost segmented welding approach is rejected in favour of customised shell wall thickness and internal reinforcement structures based on roller diameter, length, and load capacity. All extra‑long shells undergo hydrostatic and deformation simulation testing to ensure deflection remains within the allowable range under full‑load operation. Particularly suitable for BOPET, BOPE, and lithium battery separator long‑process traction sections exceeding 10 metres.
·Surface Quality Enhancement for Finished Product Yield
The ultra‑high surface finish with stable, uniform friction coefficient ensures balanced force distribution when ultra‑thin webs pass through, preventing point scratches and continuous dragging marks on separator and optical film surfaces. It reduces air entrainment between film and roller surface, minimising web flutter and deviation. The dense chrome layer resists corrosion from calcium carbonate, antioxidants, and other material additives, preventing localised pitting corrosion during long‑term use.
·Long‑Term Operational Cost Efficiency
The seamless weld‑free structure eliminates risks of weld cracking, leakage, and coating peeling along weld seams. Sufficient chrome layer thickness allows multiple re‑polishing and repair cycles without complete roller replacement. Lower vibration extends bearing and seal replacement intervals, significantly reducing unplanned production line downtime. Extra‑long dimensions are supported by professional packaging: 16‑metre rollers are shipped in custom steel framework with vacuum anti‑rust packaging, ensuring no deformation or corrosion during ocean transport.

 English